
 English
 Español
 Deutsch
 عربى
A plastic component must do more than match its individual drawing. It must locate correctly, connect reliably and fit the surrounding product. Reviewing these requirements before mold making helps manufacturers address interface risks while the design is still easier to change.
A controller housing may pass dimensional inspection but resist closing around its internal components. A trim panel may fit at one mounting point while leaving an uneven gap at another. A snap connection may engage successfully once but become damaged during servicing.
Such problems do not always come from an incorrectly manufactured part. They can also arise when individual component requirements fail to describe the complete assembly. For OEM buyers, bringing assembly information into the tooling discussion creates a clearer basis for design review, sampling and production approval.
1. Single-Part Inspection Does Not Describe the Whole Assembly
A component drawing defines important requirements, but the finished product depends on relationships between several parts. Mating surfaces, fastener positions and internal clearances must work together, including when individual components vary within their permitted tolerances.
Consider a plastic cover mounted over a metal frame. Checking the cover's overall width does not establish whether its locating features align with the frame, whether screws can enter freely or whether the visible edges sit evenly after tightening.
Before tooling begins, identify which requirements belong to the individual part and which must be verified on the assembly. Both should have agreed acceptance criteria.
2. Explain How the Part Locates, Connects and Operates
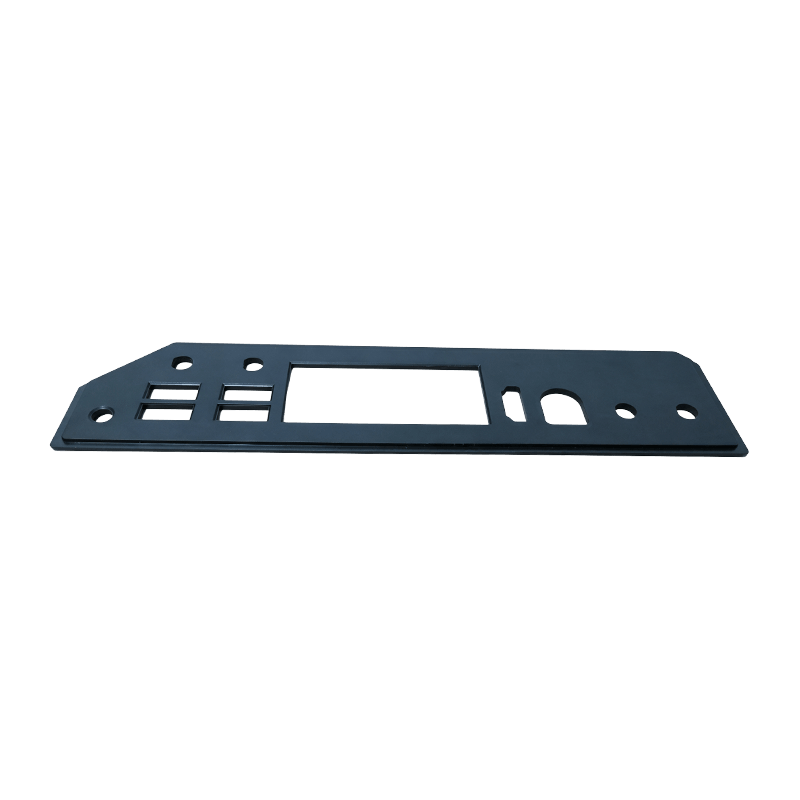
Provide an assembly drawing, mating-part models or a clear installation description alongside the part model. Identify the surfaces and features that establish position, followed by those that retain the component. These functions should be understood before detailed tooling decisions are finalized.
Explain the installation direction, available working space and access for fastening tools. A screw boss may be correctly positioned geometrically yet difficult to reach after another component is installed.
Also describe servicing requirements. A housing opened regularly needs a different review from a permanently joined cover. Moving components require clearance through their intended travel, not only in the position shown by a static model.
3. Review Connection Features Before Tool Construction
Snap-fits, screw bosses, locating pins and mounting brackets influence both assembly and mold design. Review snap engagement, available deflection space and the intended release method together with the selected material. A connection that holds firmly may still be unsuitable if installation overstresses it.
For screw bosses, clarify the fastener type, engagement arrangement and tightening requirements. Review nearby walls and ribs for their effect on strength, molding and visible-surface quality. Inserts, where required, also introduce installation and positioning requirements.
The toolmaker should evaluate how these features affect draft, undercuts, parting lines and ejection. Gate vestiges or ejector marks must not obstruct a locating surface or a close-fitting connection.
4. Check Tolerance Stack-Up Across Mating Components
Several acceptable dimensional variations can combine to produce an unacceptable assembly. In a controller enclosure, the front shell, rear shell, internal bracket and mounted electronics all contribute to the available clearance.
Review the dimensions controlling that clearance as a connected chain. Select suitable datums and identify which interfaces need the closest control. Making every dimension tighter can increase manufacturing and inspection effort without resolving a poorly defined locating arrangement.
When different suppliers produce mating components, maintain a shared interface definition and revision record. Confirm who owns each critical dimension and how compatibility will be checked. Supplier approval of an isolated component should not be treated as approval of the complete fit.
5. Evaluate Shrinkage and Warpage in the Installed Condition
Resin behavior, wall distribution, reinforcement, gate arrangement and cooling can affect the final shape of an injection molded component. Long mating edges and broad covers deserve particular attention because shape variation can become visible across the assembled product.
Agree whether critical geometry will be inspected freely, in a defined fixture or on representative mating parts. Record the support and fastening conditions so measurements are repeatable. Where conditioning time or environmental conditions matter, include them in the inspection plan.
Some flexible panels are designed to locate during normal fastening. That allowance must be intentional and bounded. Excessive force, distorted surrounding parts or overstressed connections should not become an informal method for achieving assembly acceptance.
6. Include Painting and Finishing in the Fit Review
When plastic parts will be painted, assess the delivered surface condition during assembly planning. Coating on mating faces can change clearances, while coating near clips or locating features may affect engagement or become damaged during installation.
Mark areas requiring masking, including selected holes, contact surfaces and close-fitting interfaces. Clarify which dimensions apply to the molded part and which apply after finishing. Where coating thickness is functionally important, define its requirement and verification method.
Assembly trials should include the specified finishing condition before final approval. Also review how operators handle visible surfaces, where fixtures contact the part and whether installation could scratch adjacent painted components. Successful assembly of an unfinished sample does not establish acceptance of the finished product.
7. Plan Physical Validation Before Mass Production Approval
Digital assembly checks help identify interference and access problems. Moldflow analysis can support evaluation of filling behavior and potential molding risks. Neither establishes every aspect of physical assembly performance.
Use trial-molded parts with representative mating components to check location, closure, fastening, gaps and flushness. Where servicing is required, include opening and reassembly checks appropriate to the intended use. Record any installation force or tightening limits that determine acceptance.
Document the drawing revision, resin, processing condition and finishing status of the samples. Prototype or unfinished components can support early learning, but their limitations should remain visible in the approval record.
Close agreed corrective actions and obtain the necessary approvals before releasing production. If a design or manufacturing change affects an interface, review whether assembly validation must be repeated.
A Pre-Tooling Assembly Review Checklist
| Review area | What to confirm before mold making |
|---|---|
| Mating information | Current models, drawings, representative samples and interface responsibilities |
| Location and access | Datums, installation direction, locating sequence and fastening-tool access |
| Connection features | Snap engagement, screw bosses, inserts, mounting features and service needs |
| Dimensional relationships | Critical tolerances, accumulated variation, clearances and measurement methods |
| Molding considerations | Shrinkage, warpage, draft, undercuts, gate locations and ejection |
| Surface finishing | Coating boundaries, masking areas and fit after finishing |
| Validation and release | Sample condition, assembly checks, acceptance criteria and approval responsibilities |
Bring Assembly Information into the First Supplier Discussion
An effective review starts before the mold is built. Share the part model together with its assembly context, expected service conditions and critical interfaces. If some mating components are still being designed, list those interfaces as open items rather than allowing assumptions to become tooling decisions.
Purchasing teams can help by connecting product engineers, mating-part suppliers and manufacturing personnel early. Record agreed actions, responsible owners and the design revision used for tooling release. This keeps a commercial quotation, engineering review and production plan aligned around the same product requirements.
Kaidi combines mold making, injection molding, surface painting and assembly support. For custom housings, covers, trim panels and brackets, providing the assembly information at the inquiry stage helps define which interfaces need review and which checks should be included in sampling.
Send the available drawings, mating-part information and required delivery condition to begin evaluating the project as a complete manufacturing and assembly task.